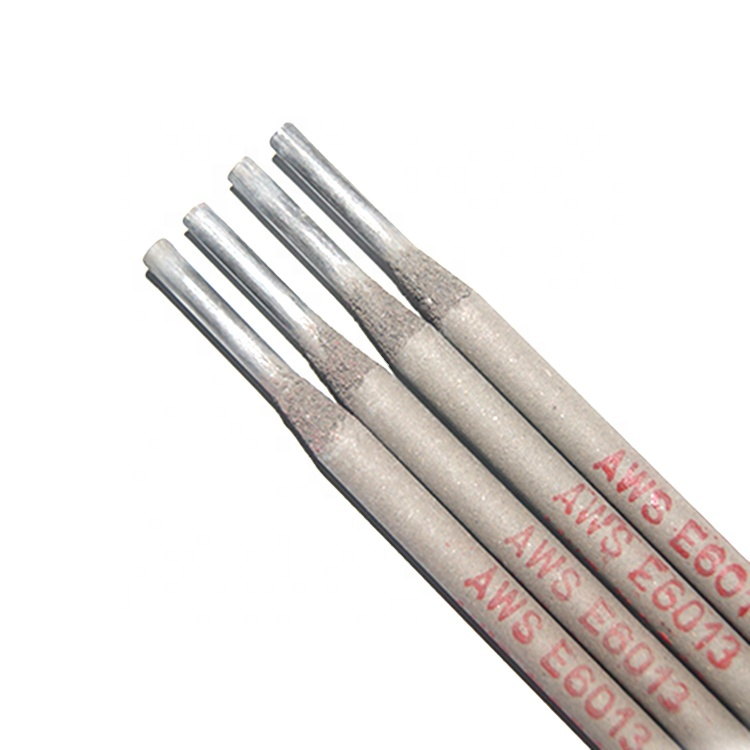
E6013 Mild Steel Welding Electrode
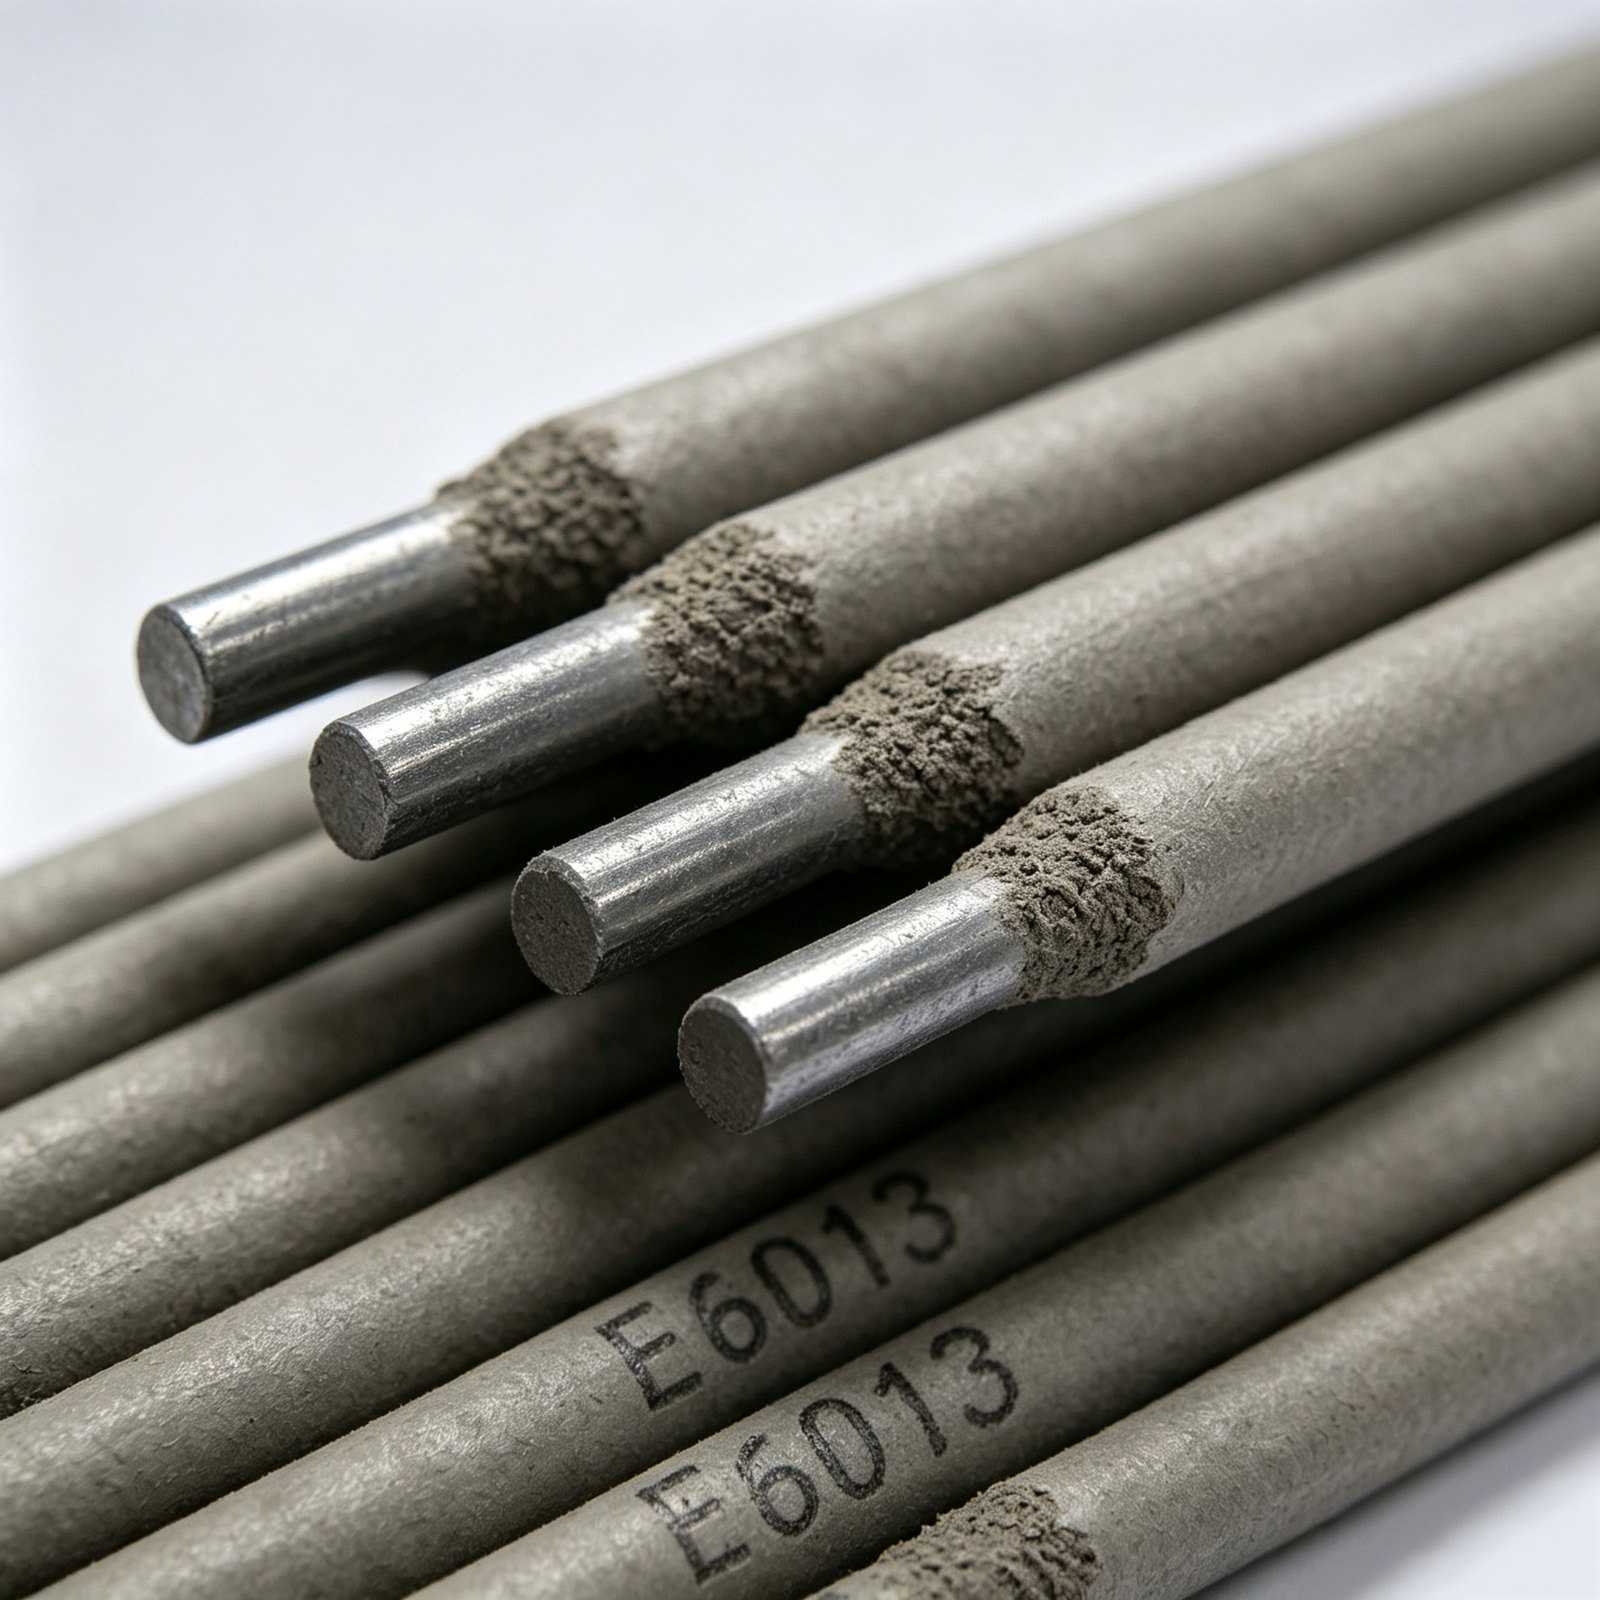
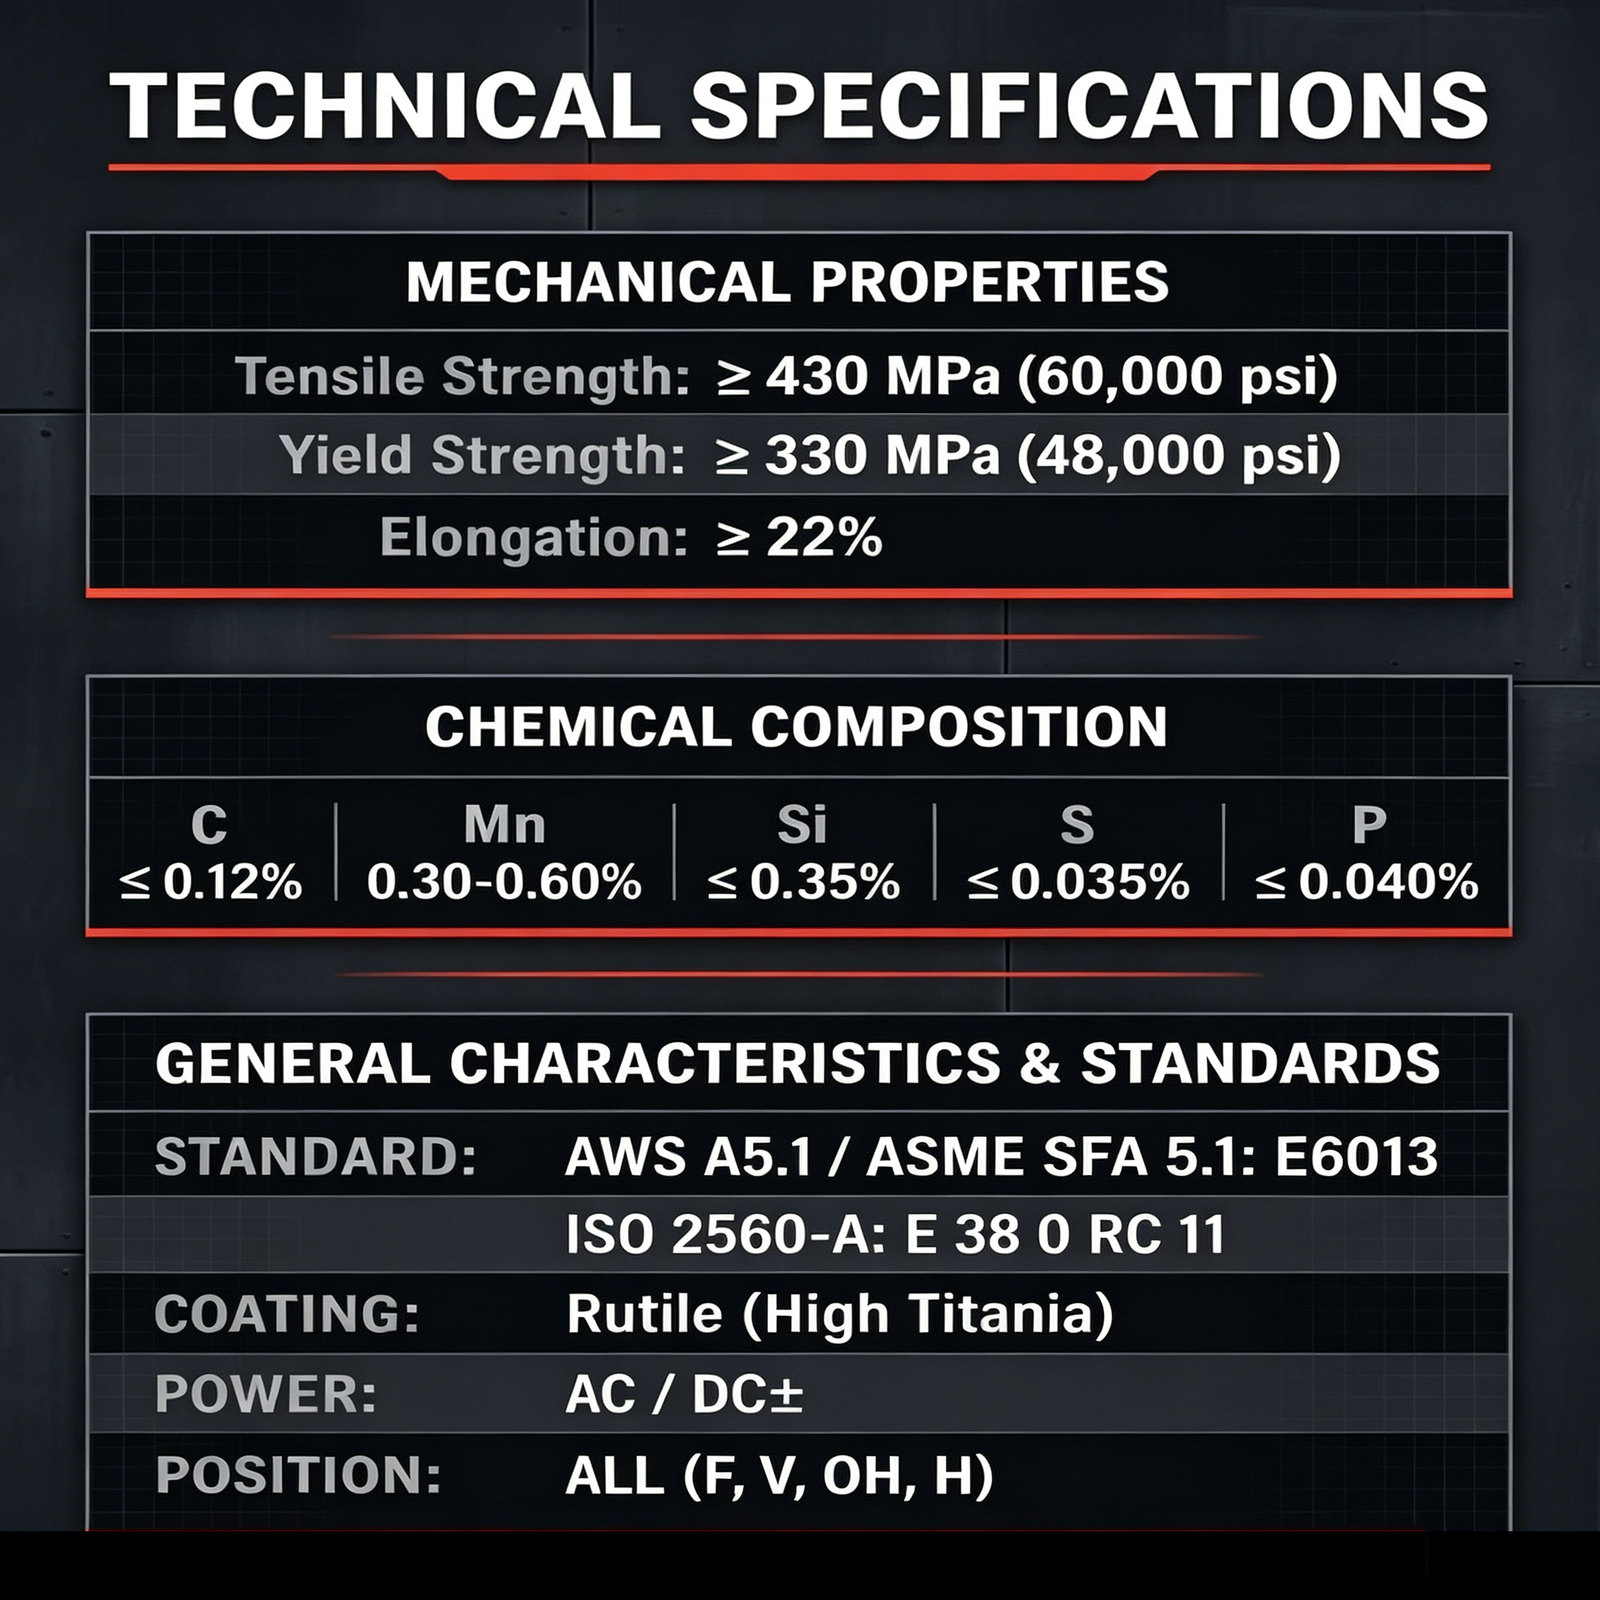
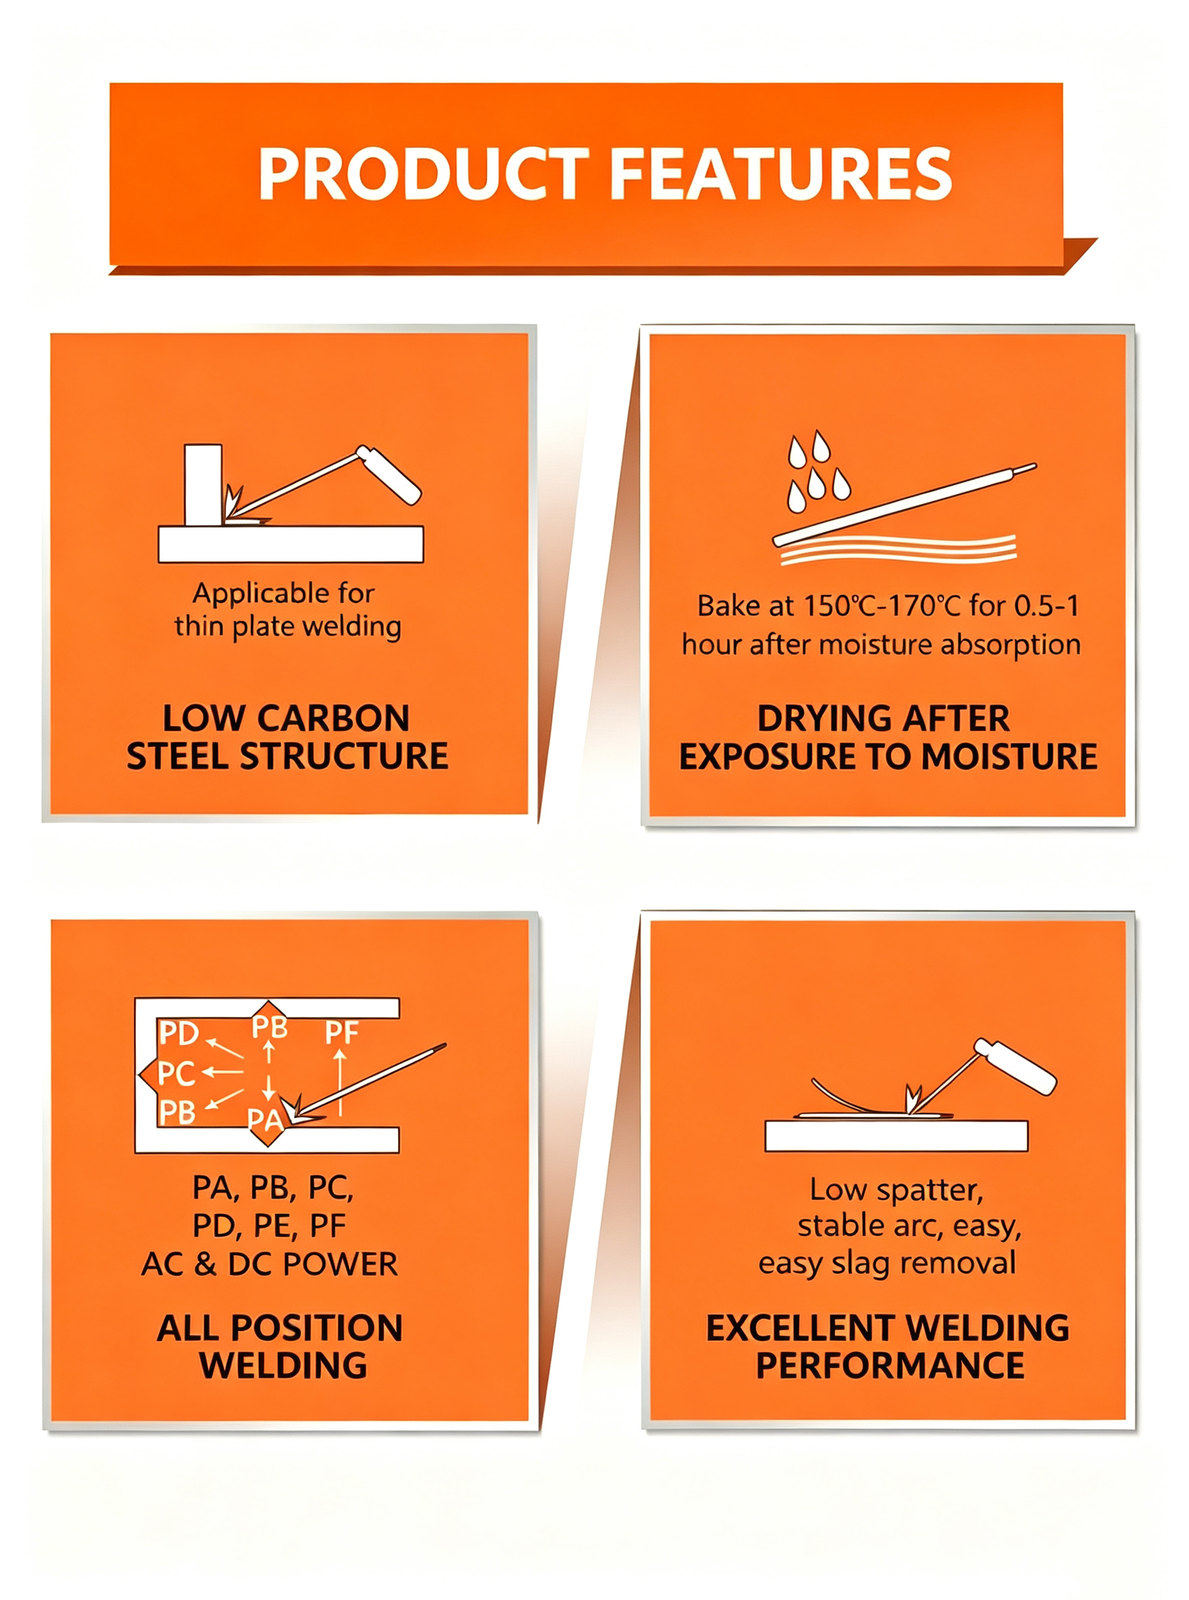
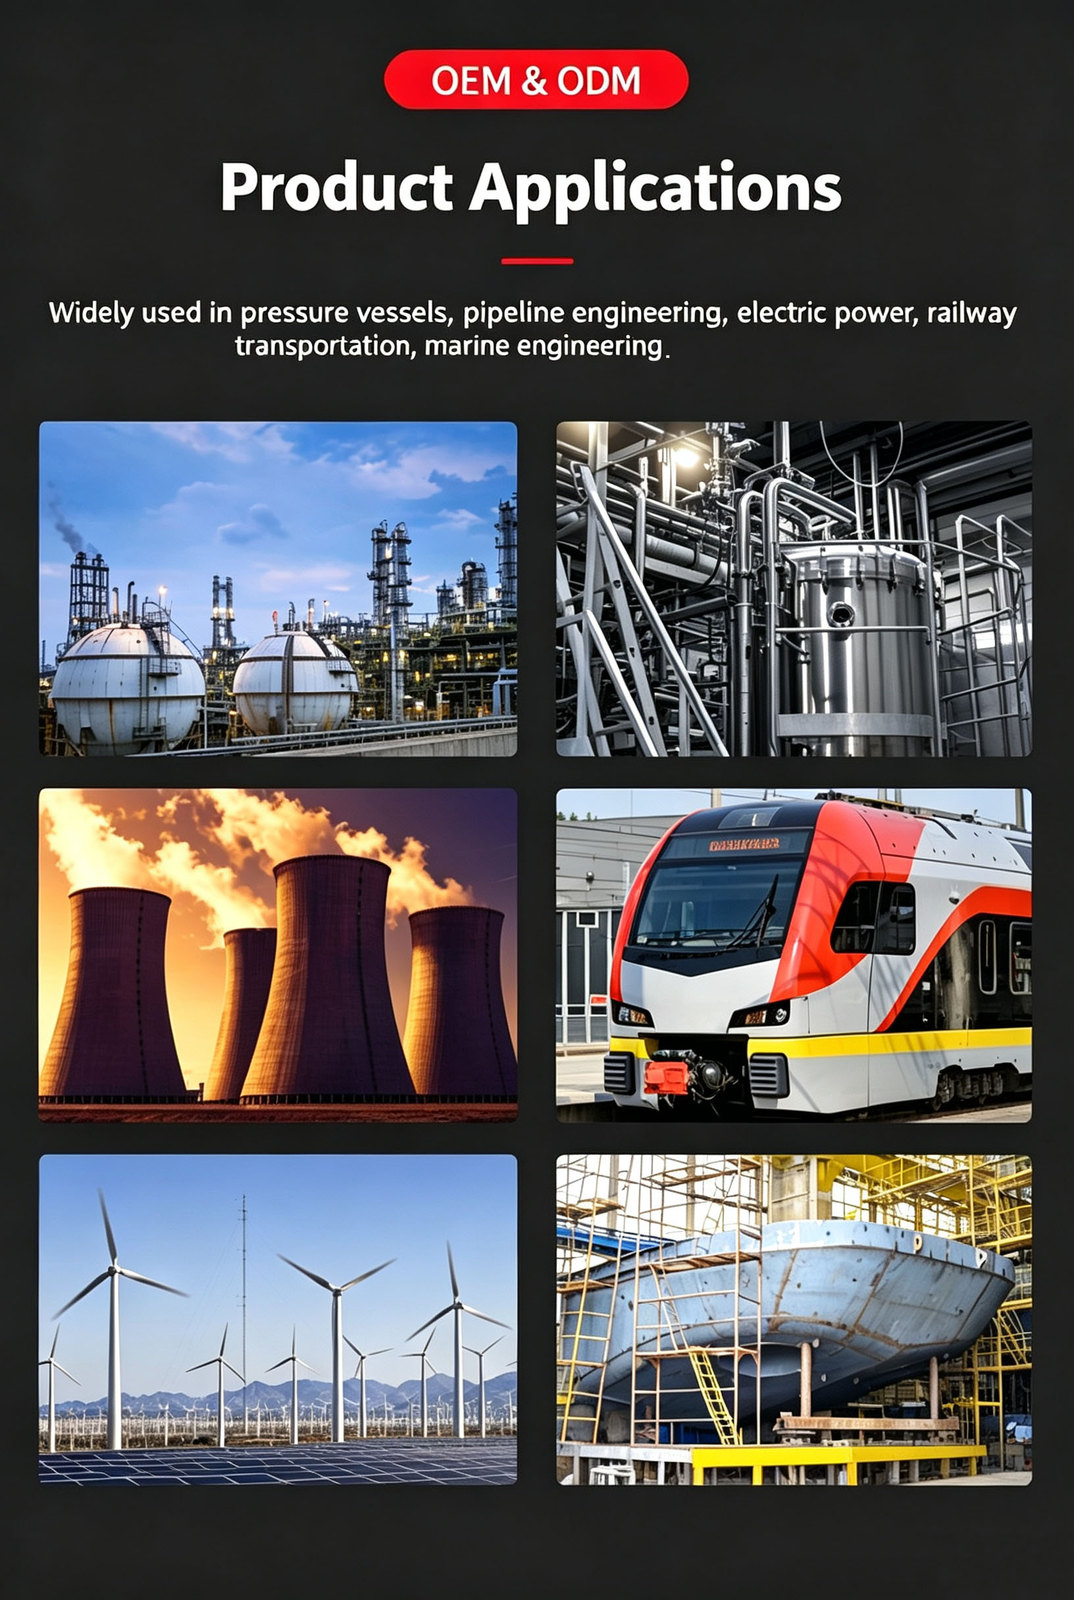
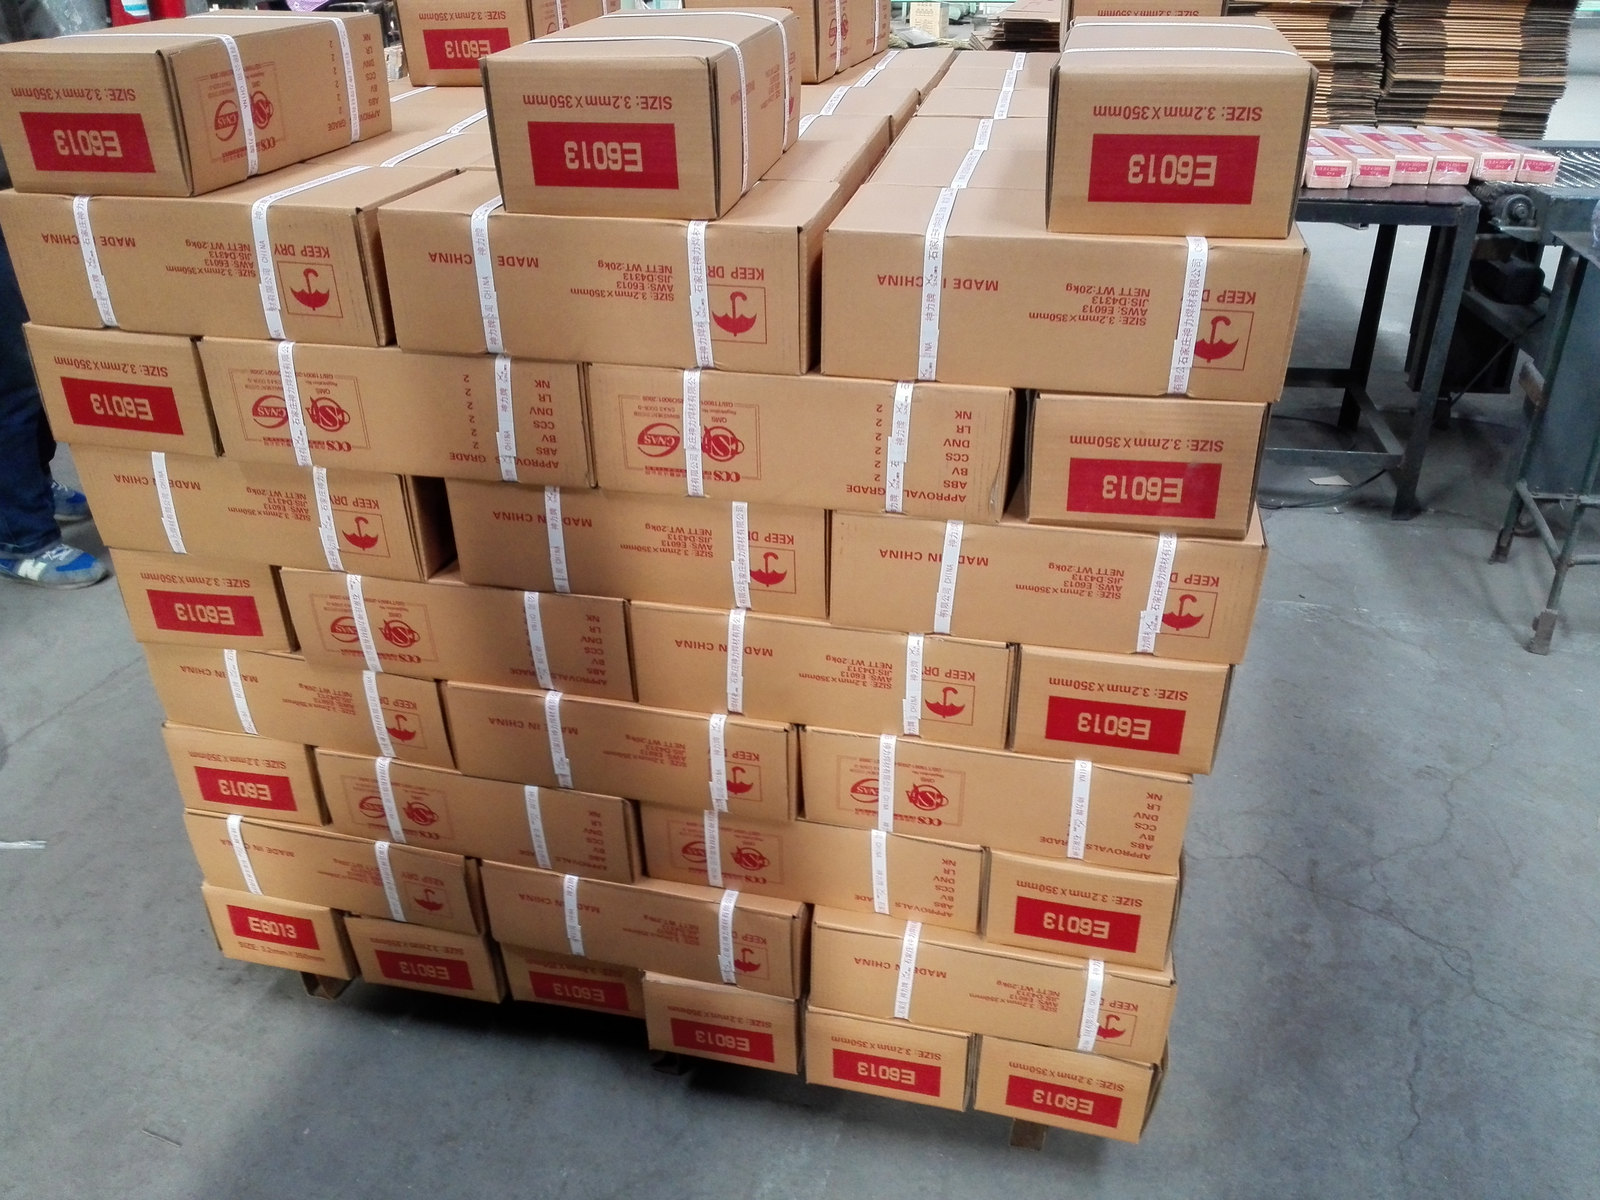
E6013 is a rutile-coated mild steel electrode supplied to AWS A5.1, used for general fabrication, structural steel, thin sheet, repair work and pressure-vessel joints on carbon steel. It runs on either AC or DC, and the catalogue stocks it in 2.0 mm, 2.5 mm, 3.2 mm, 4.0 mm and 5.0 mm diameters, packed 5 kg to an inner box and 20 kg to a carton.
Status
Datasheet available on request
Description
Rutile-type mild steel electrode.
Welding positions, current range, deposition data and procedure notes are provided with the datasheet. Ask us for the grade you are specifying.
- Diameter
- 2.0mm, 2.5mm, 3.2mm, 4.0mm, 5.0mm
- Material
- Carbon steel
- Packing
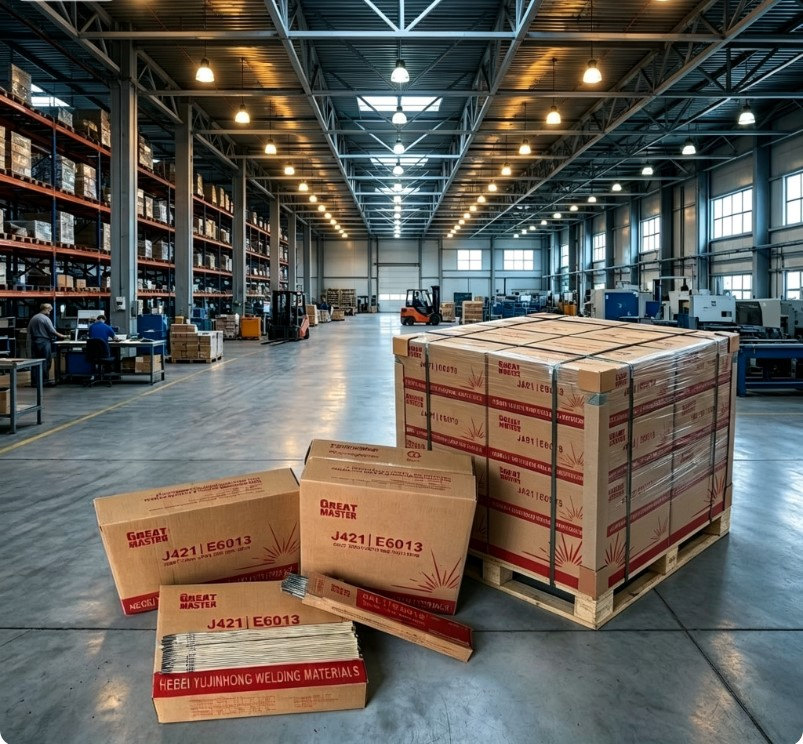
- 5kg/inner box, 20kg/carton; or as per customer request
- Standard
- AWS A5.1 E6013
- Application
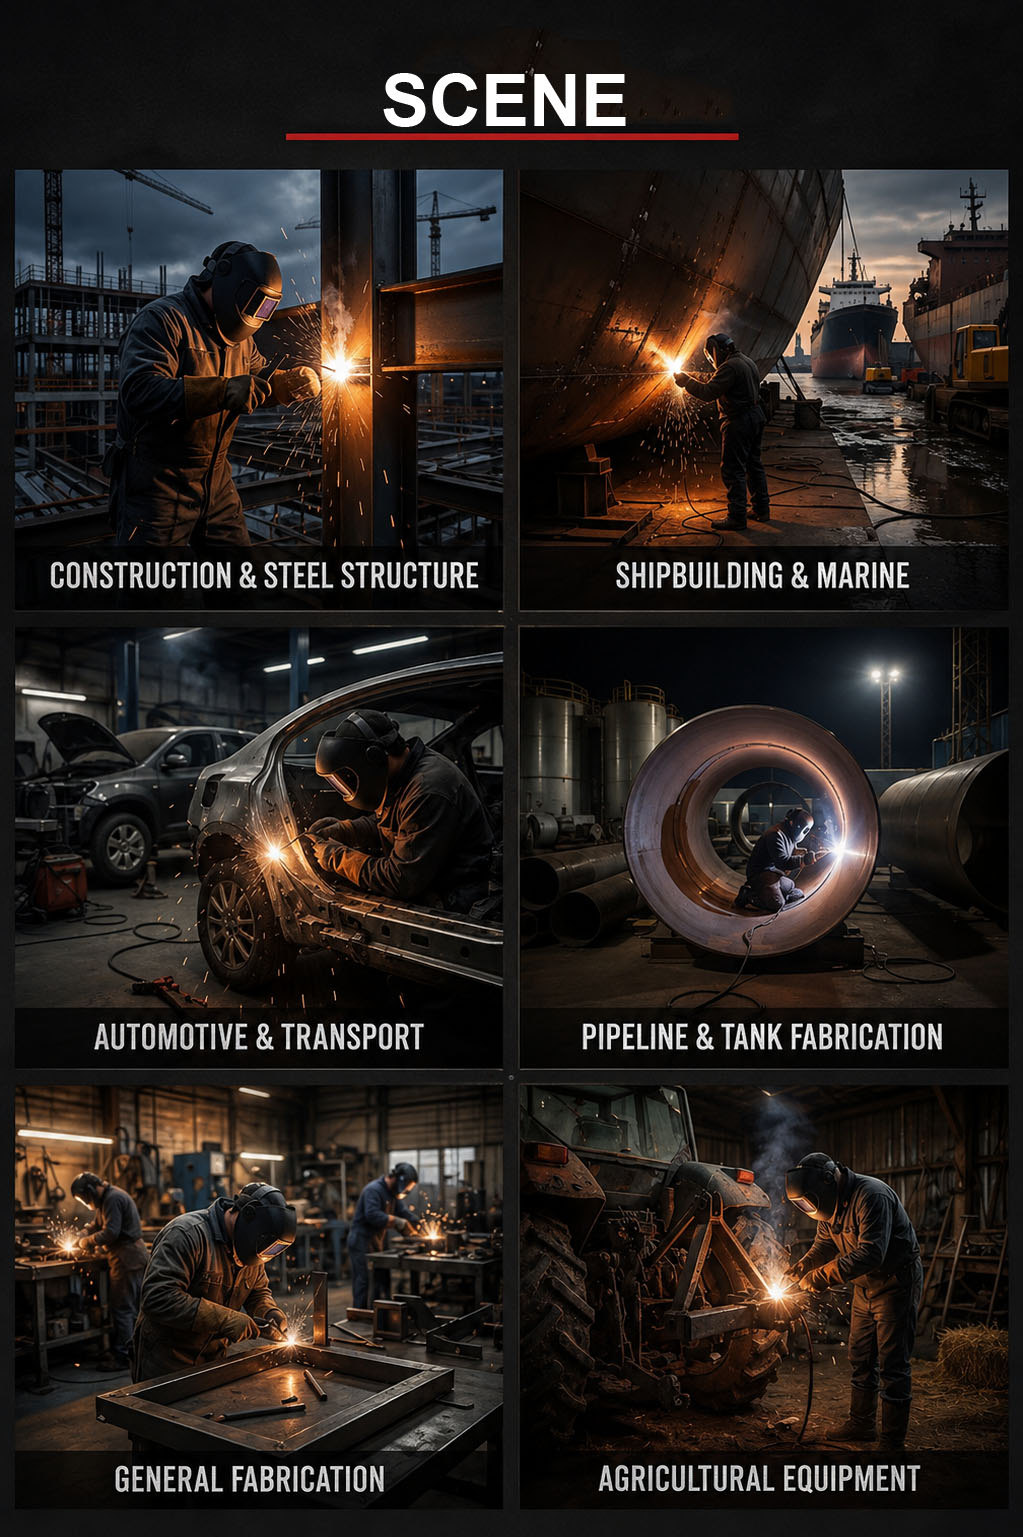
- Stainless Steel Welding, Pipeline Welding, Shipbuilding Welding, Carbon Steel Welding, Structural Steel Welding, Pressure Vessel Welding, Repair and Patch Welding, Thin Sheet Welding, Indoor/Outdoor Structural Welding
- Form / model
- E6013
- Welding current
- AC, DC
- Operating temperature
- 800°C(1440℉)
- MOQ
- 2 Tons
- Selling unit
- Single item
- Single gross weight
- 1.050 kg
- Single package size
- 40X8X8 cm
Lead time
- 1 - 3,000
- 15 days
- 3,001 - 5,000
- 30 days
- > 5,000
- To be negotiated days
What is E6013 welding electrode used for?
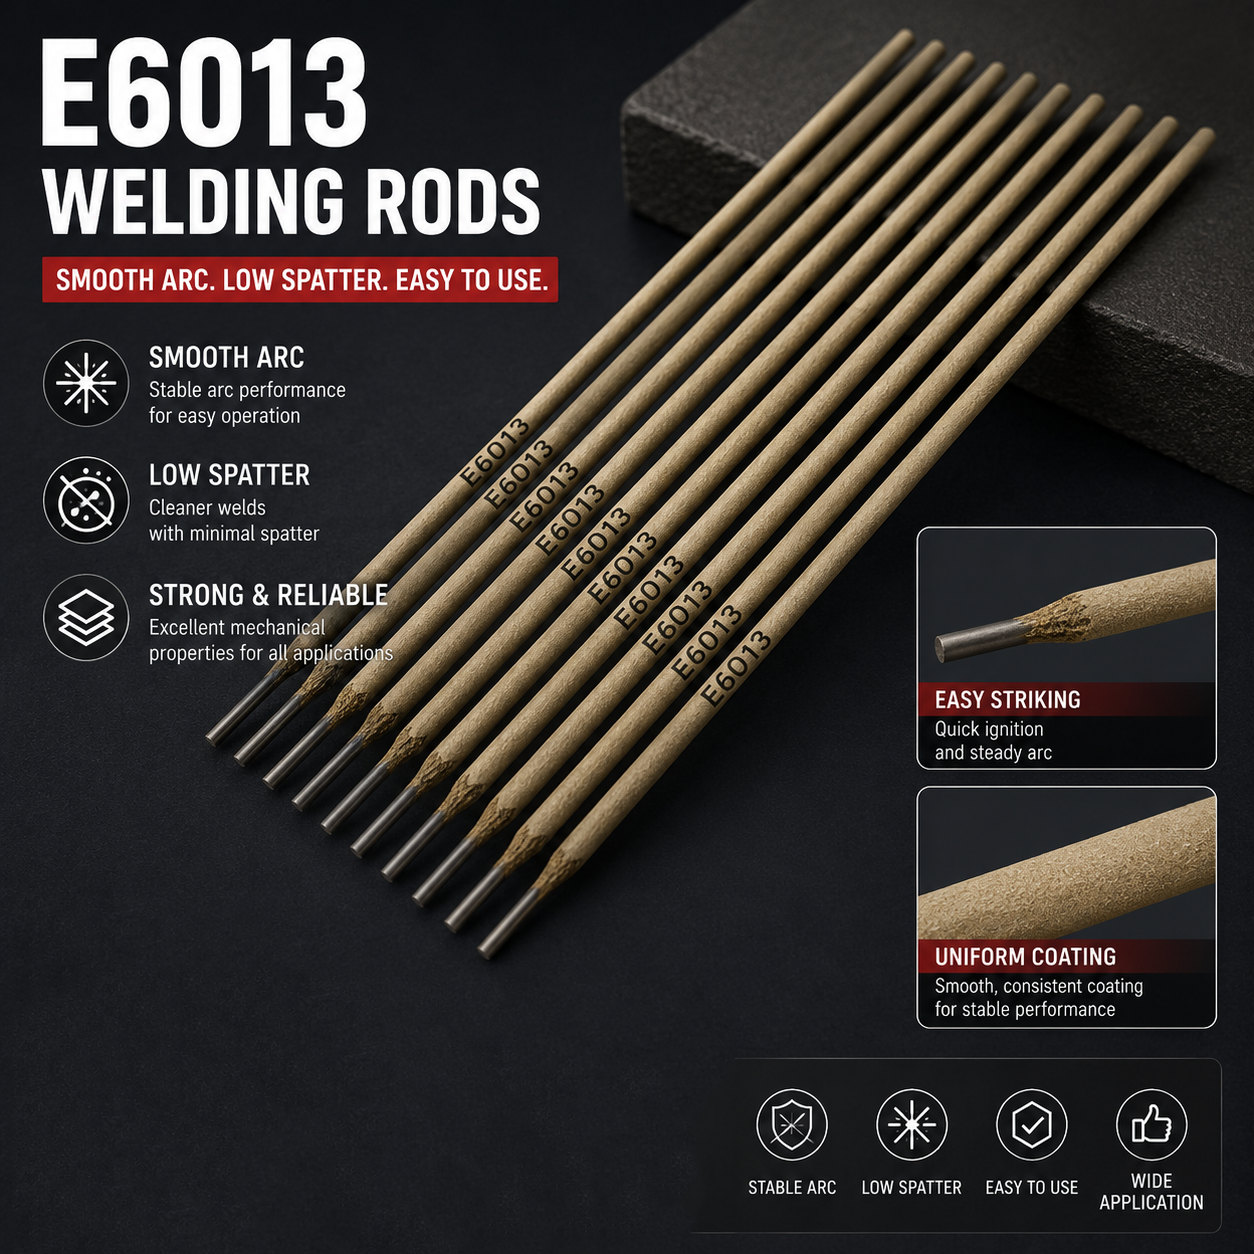
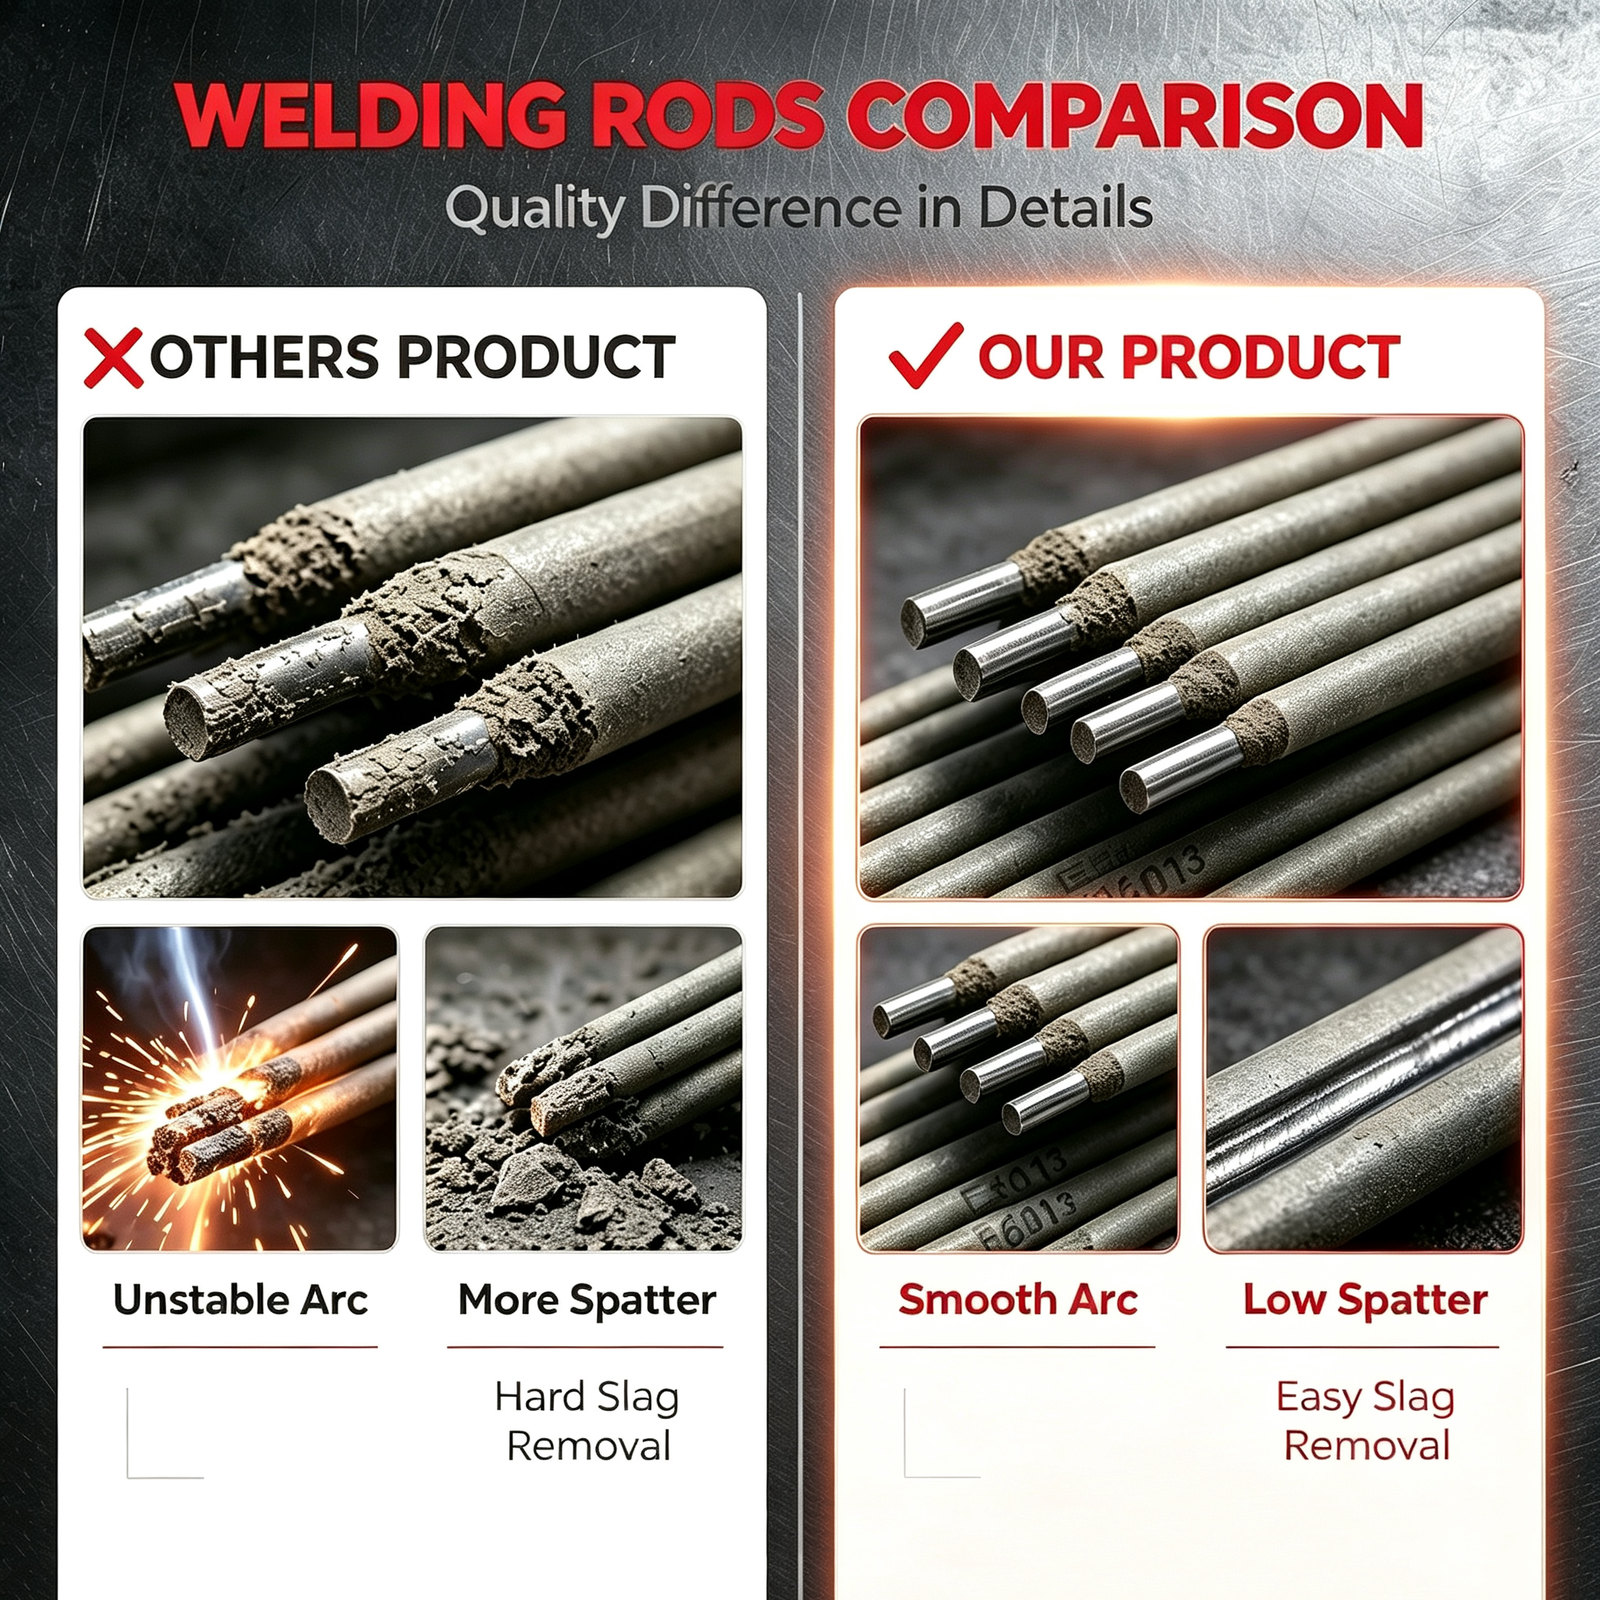
E6013 is a rutile-coated, all-position carbon steel electrode ideal for general fabrication, structural steel, sheet metal work, shipbuilding, automotive repair, and light-to-medium industrial welding. It delivers smooth arc performance with minimal spatter and easy slag removal.
Can E6013 be used on AC and DC?
Yes. E6013 is compatible with both AC and DC power sources (DCEP or DCEN). Its rutile coating with potassium compounds ensures stable arc ignition even on low open-circuit voltage (OCV) AC machines.
What is the difference between E6013 and E7018?
E6013 offers smoother arc and easier slag removal ideal for general fabrication and thin-to-medium sheet metal. E7018 has higher tensile strength (≥70,000 psi) and low-hydrogen coating, making it better for structural and high-strength applications. E6013 is the more cost-effective, all-purpose choice.
How do you ensure consistent quality across batches?
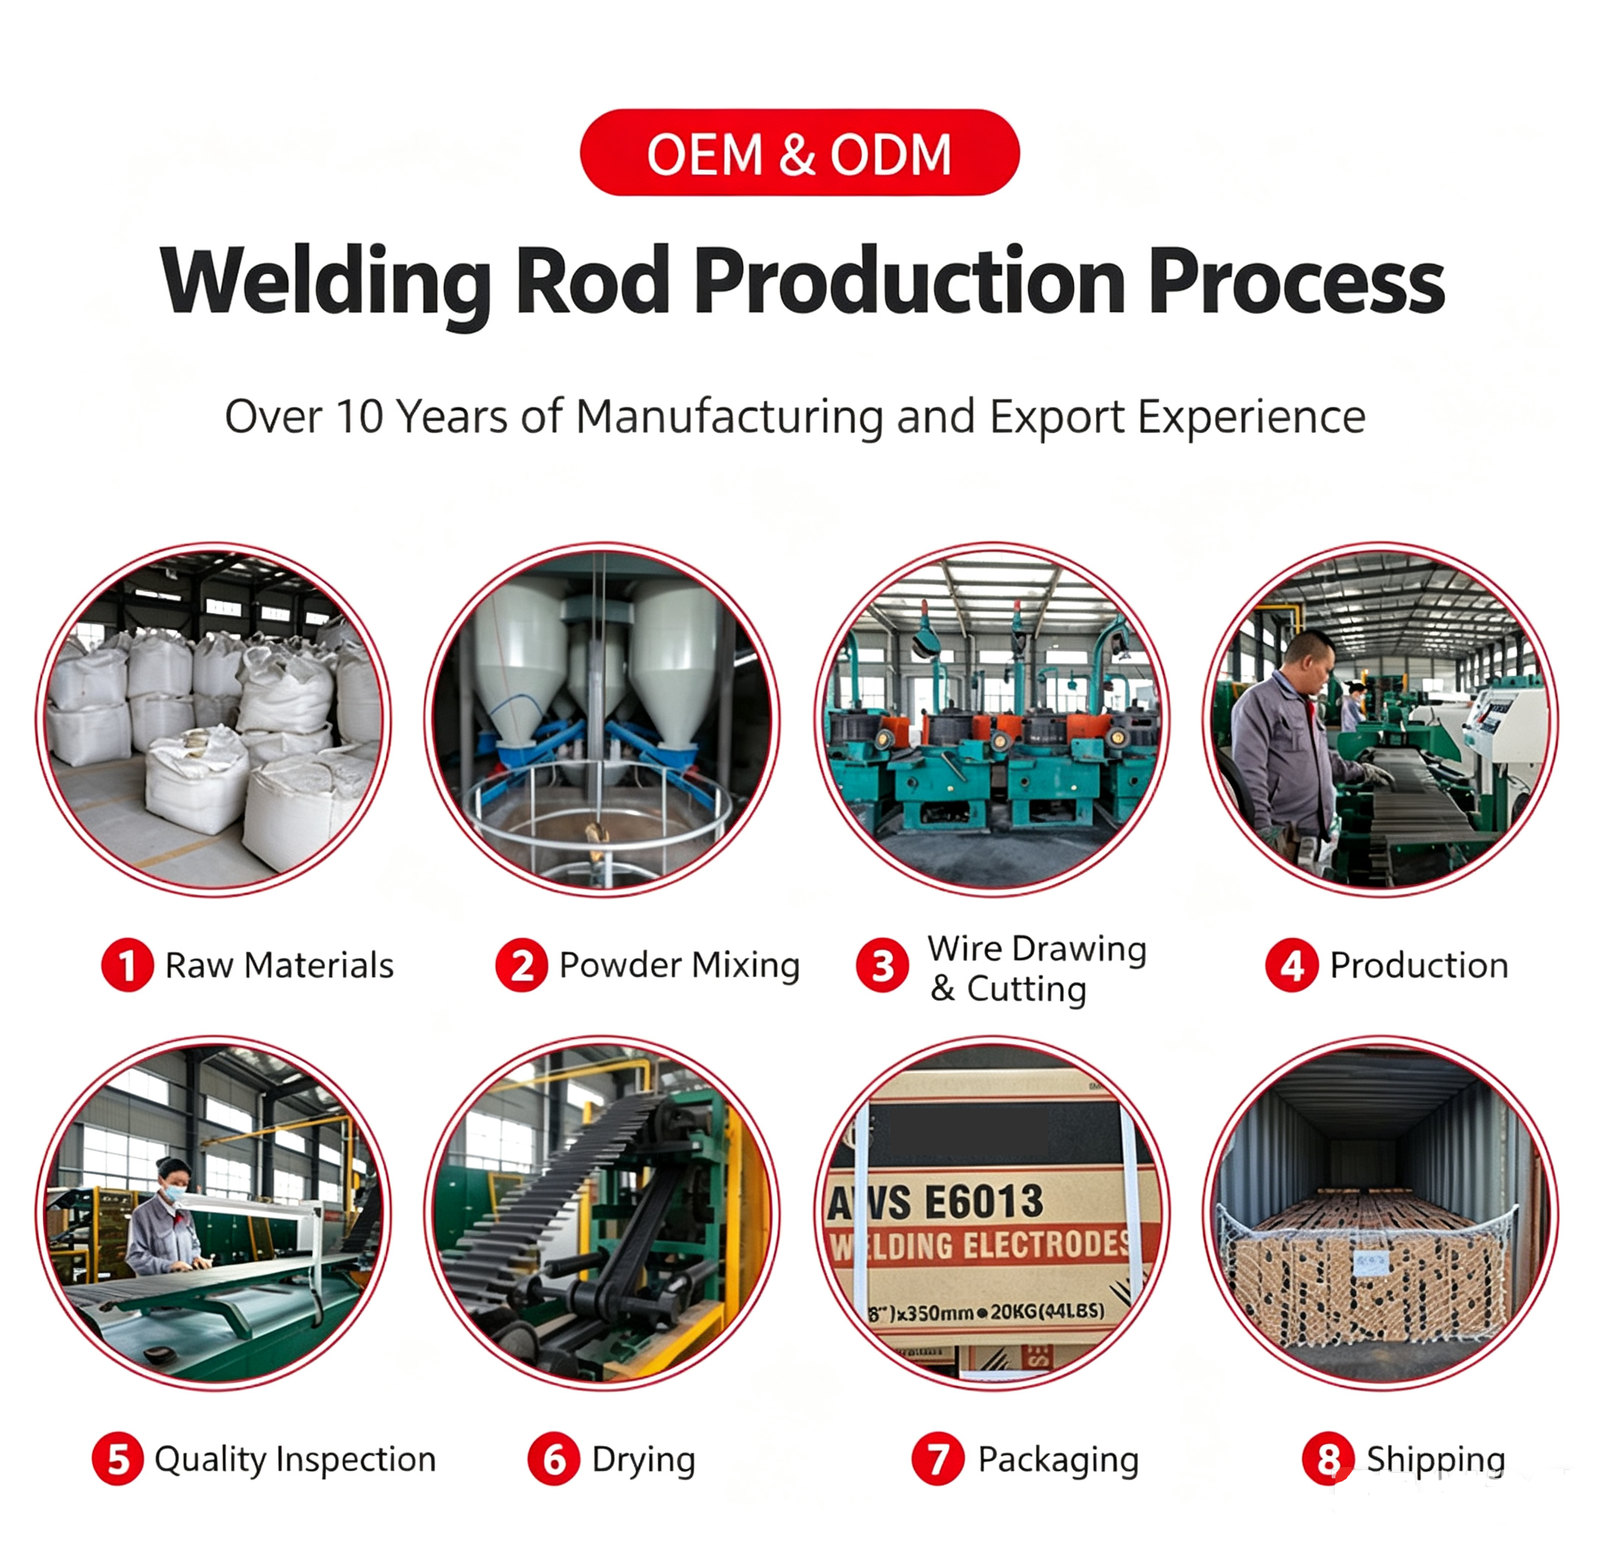
Every production batch undergoes: Chemical composition analysis (spectrometer); Tensile & yield strength testing; Arc performance & spatter evaluation; Slag removal & bead appearance inspection. Third-party inspection (SGS, BV, Intertek) available upon request.
Other grades in this family
E6024 Iron Powder Welding Electrode
Iron powder electrode for flat and horizontal work.
View grade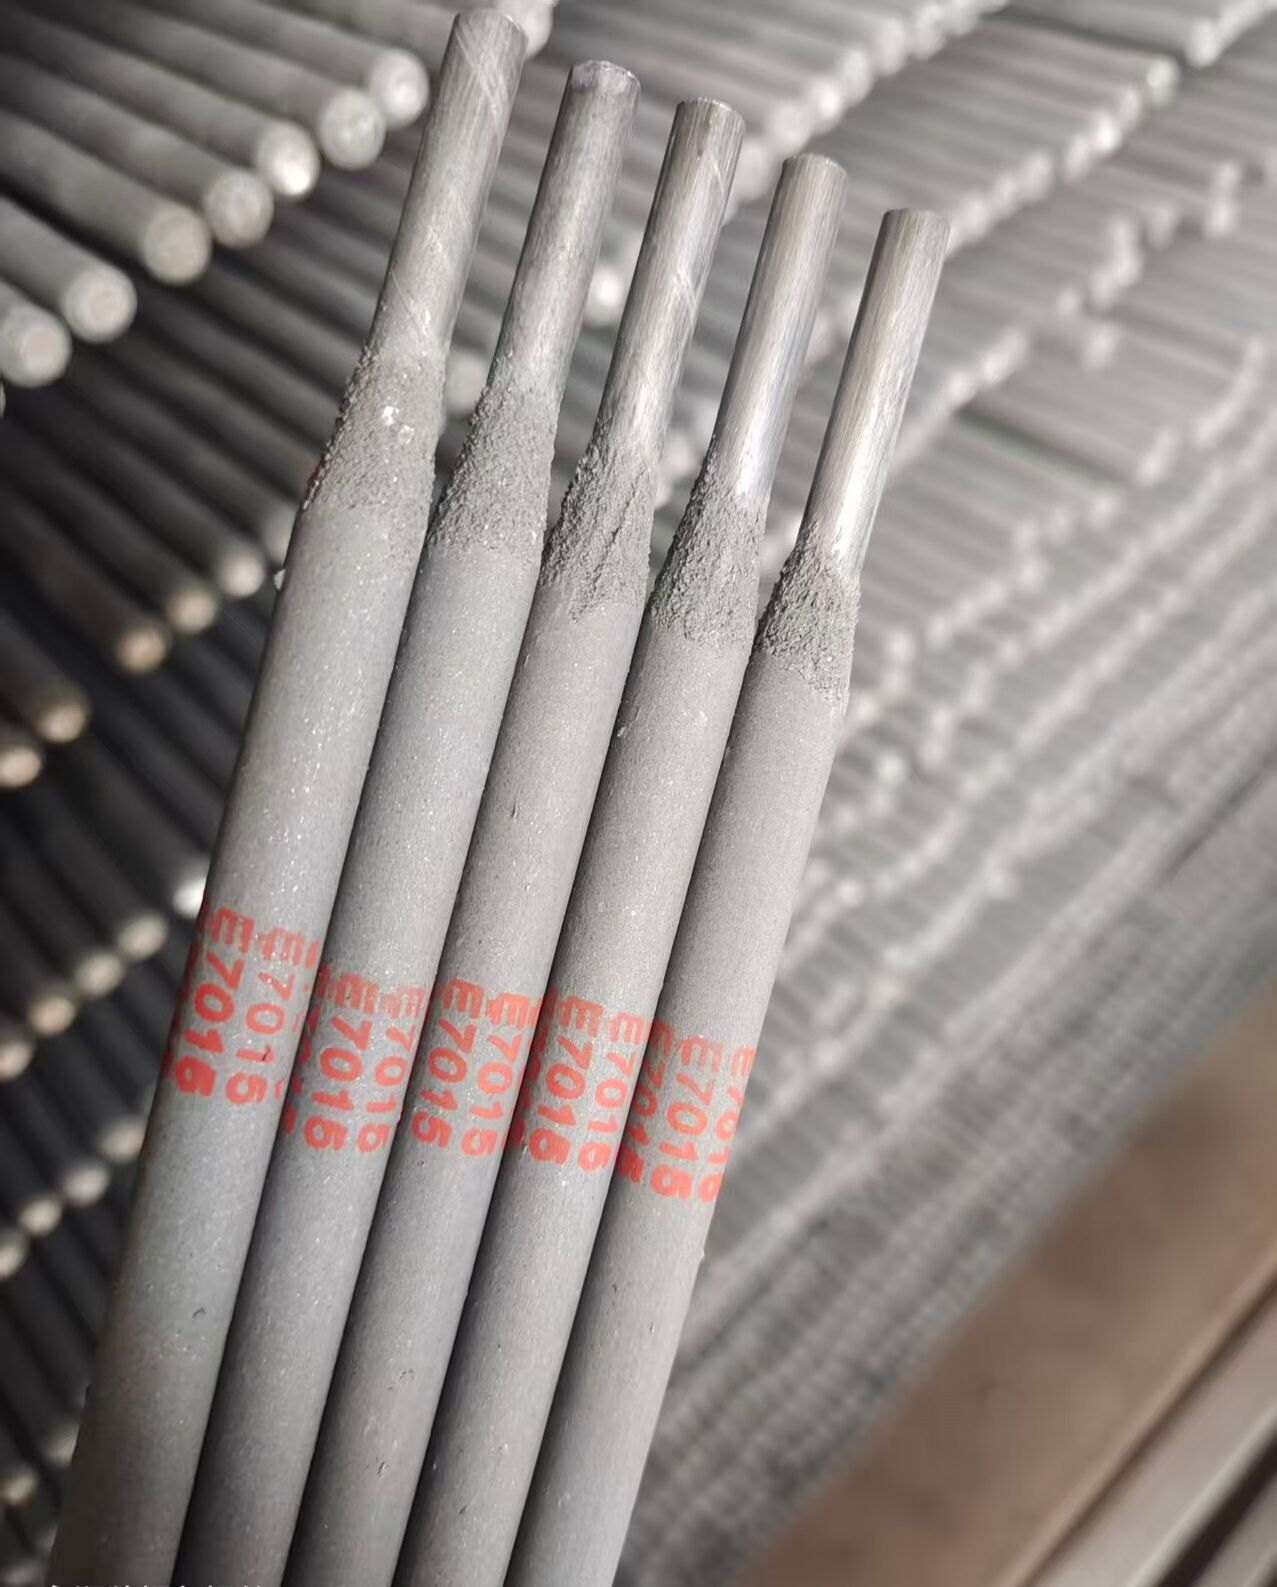
E7015 Low-Hydrogen Welding Electrode
Low-hydrogen electrode for all-position work.
View grade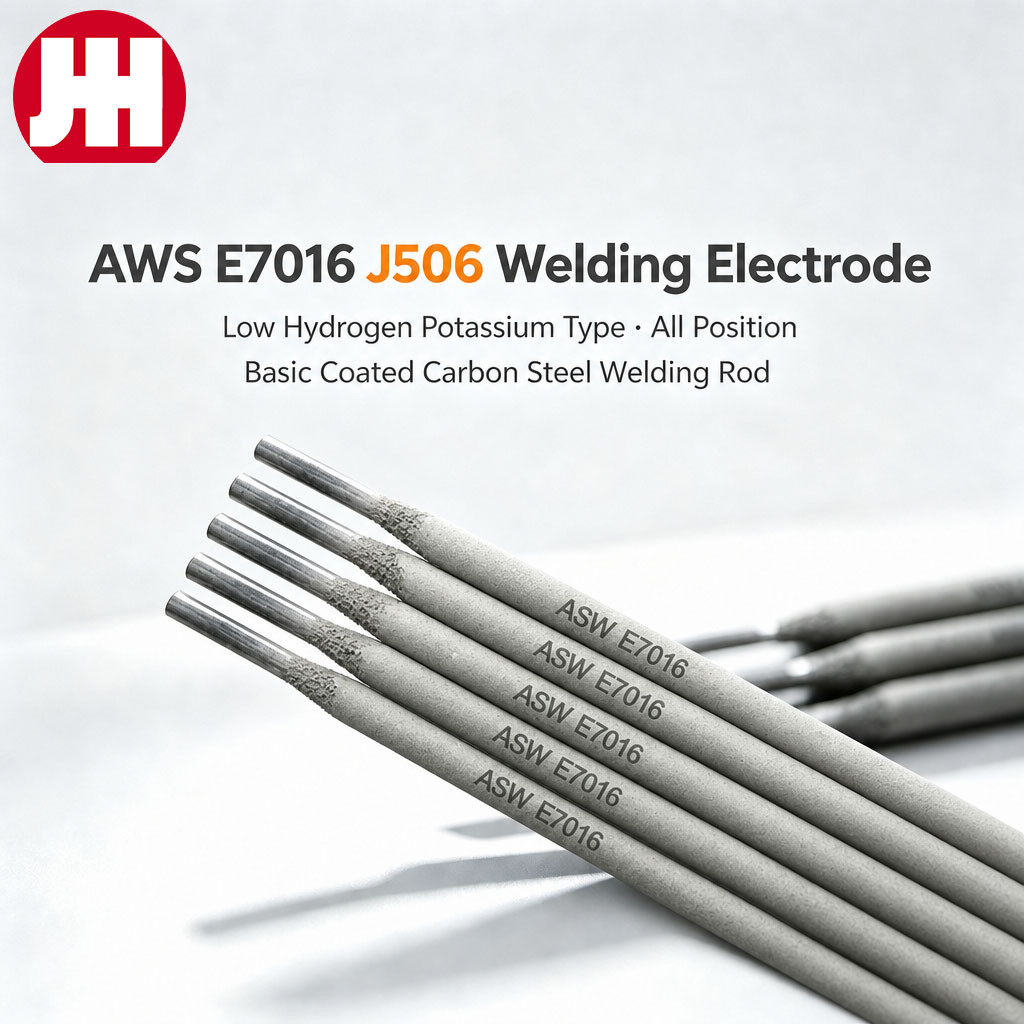
E7016 Low-Hydrogen Welding Electrode
Low-hydrogen electrode for all-position work.
View grade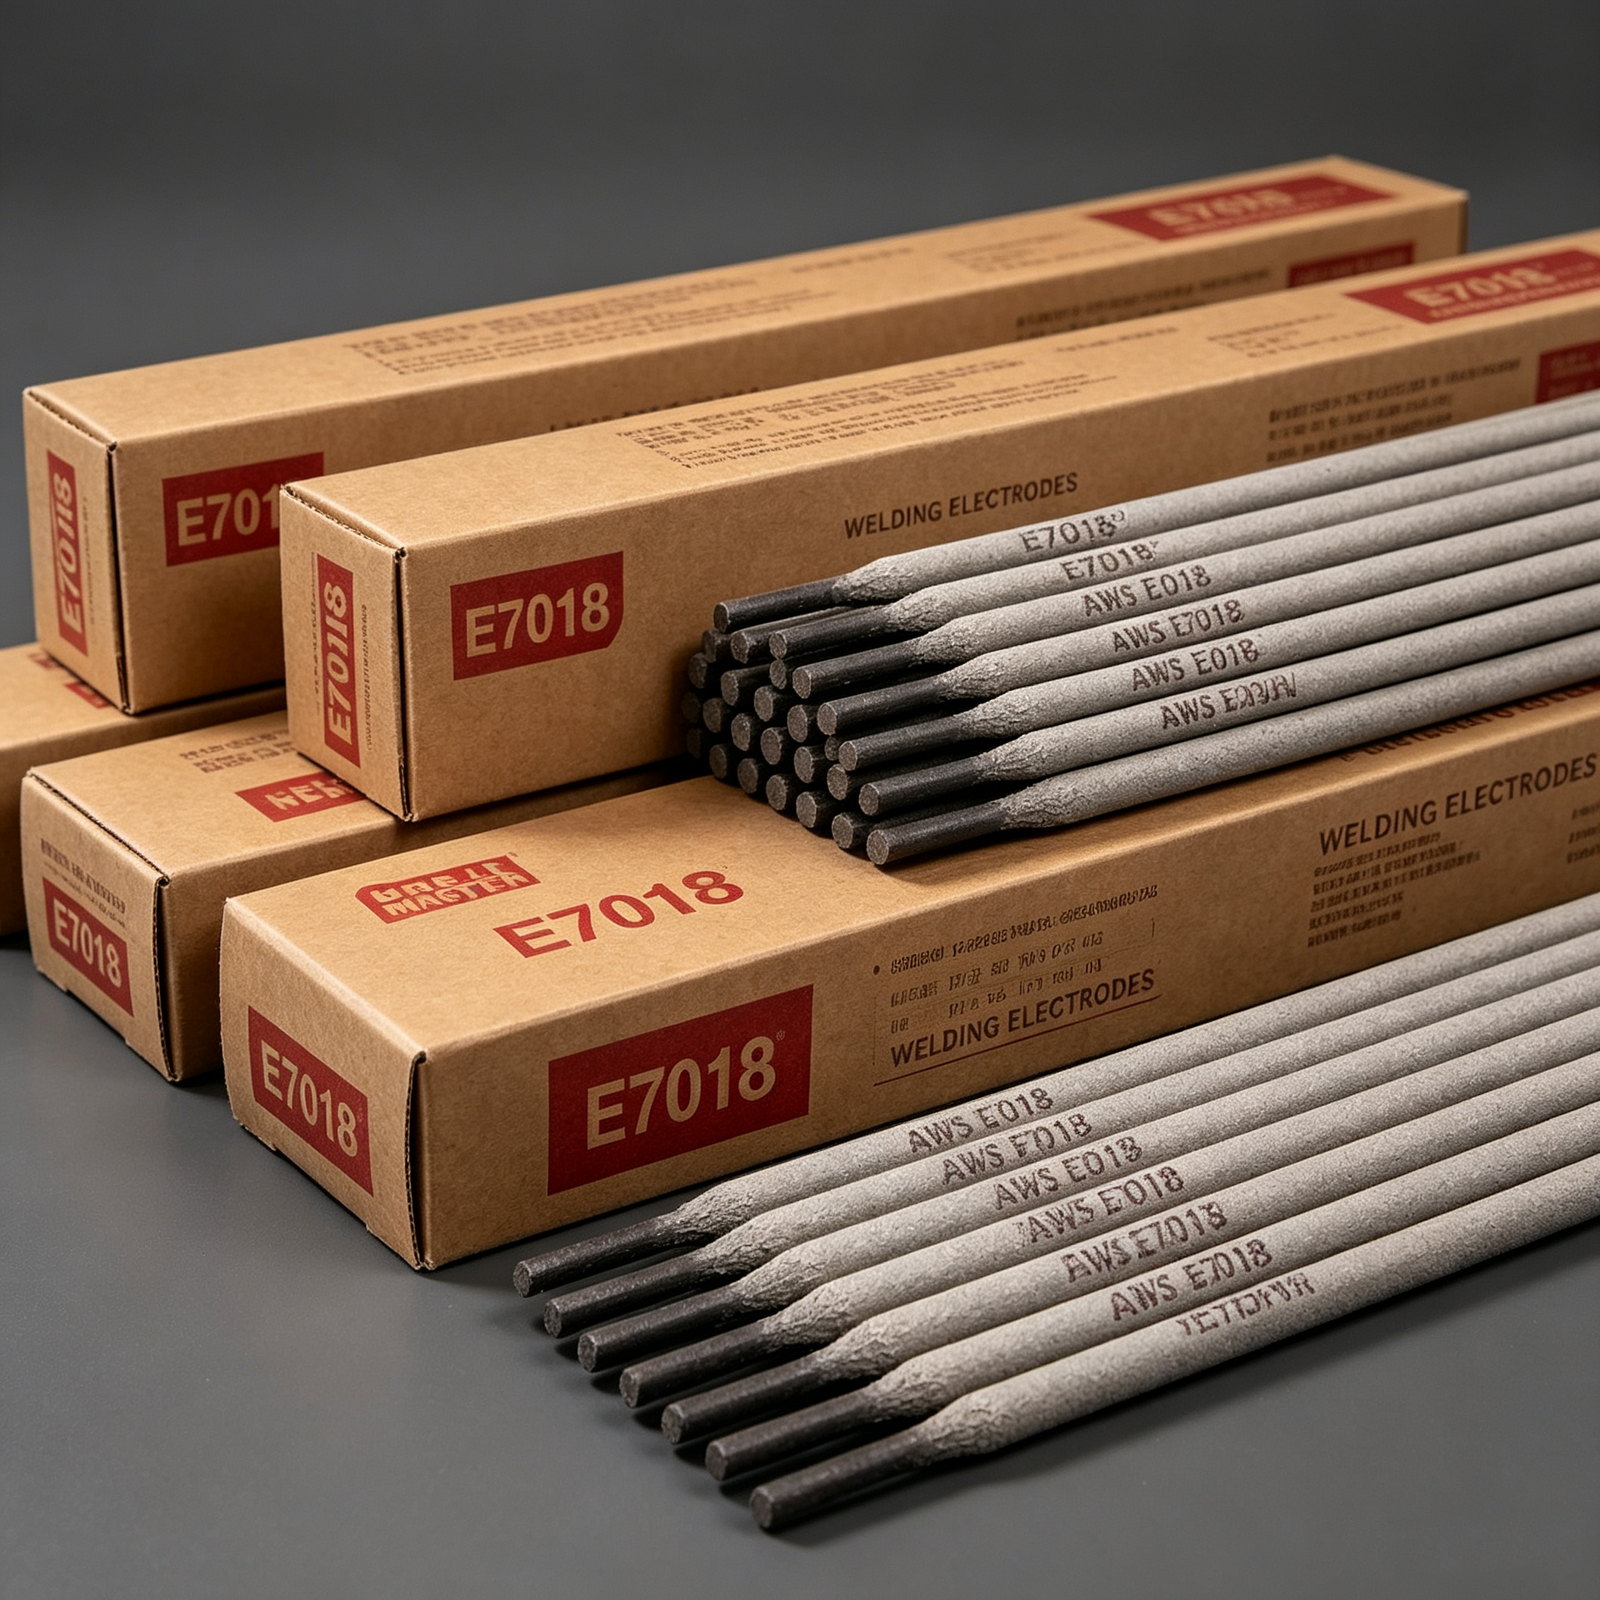
E7018 Low-Hydrogen Welding Electrode
Low-hydrogen iron powder electrode.
View grade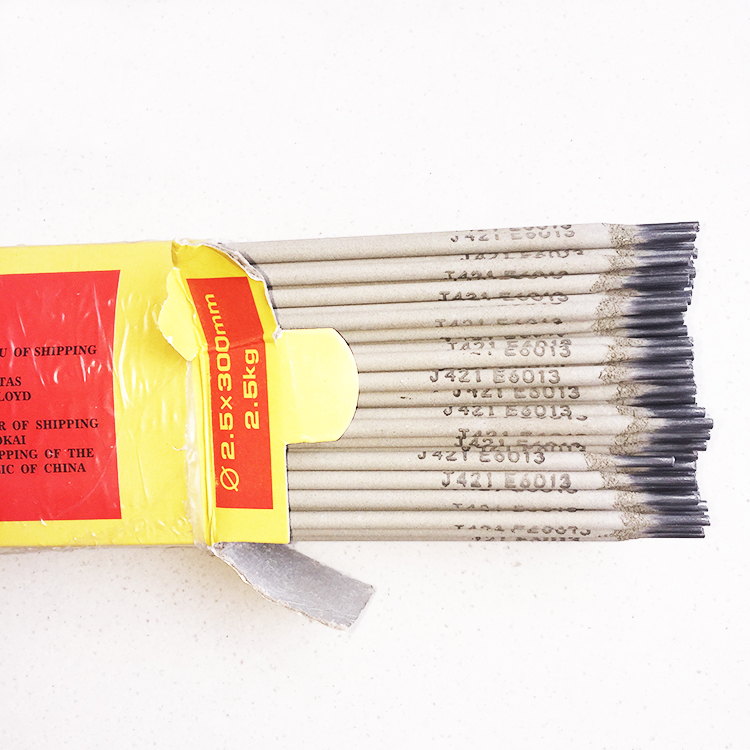
E7024 Iron Powder Welding Electrode
Iron powder electrode for flat, high-deposition work.
View grade
E7028 Iron Powder Low-Hydrogen Electrode
Iron powder low-hydrogen electrode.
View grade